Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 1
Indicate whether the statement is true or false.
1. Control limits for the s-chart are given by: LCLs = B3s and UCLs = B4s, where B3 and B4 are constants.
a.
True
b.
False
2. The frequency of sampling in pre-control is often determined by dividing the time period between two successive out-
of-control signals by six.
a.
True
b.
False
3. Control limits for variables and attributes data utilize different mathematical formulas.
a.
True
b.
False
4. In determining the method of sampling, samples should be chosen to be as heterogeneous as possible so that each
sample reflects the system of common causes or assignable causes that may be present at that point in time.
a.
True
b.
False
5. Pre-control should only be used when process capability is no greater than 88 percent of the tolerance.
a.
True
b.
False
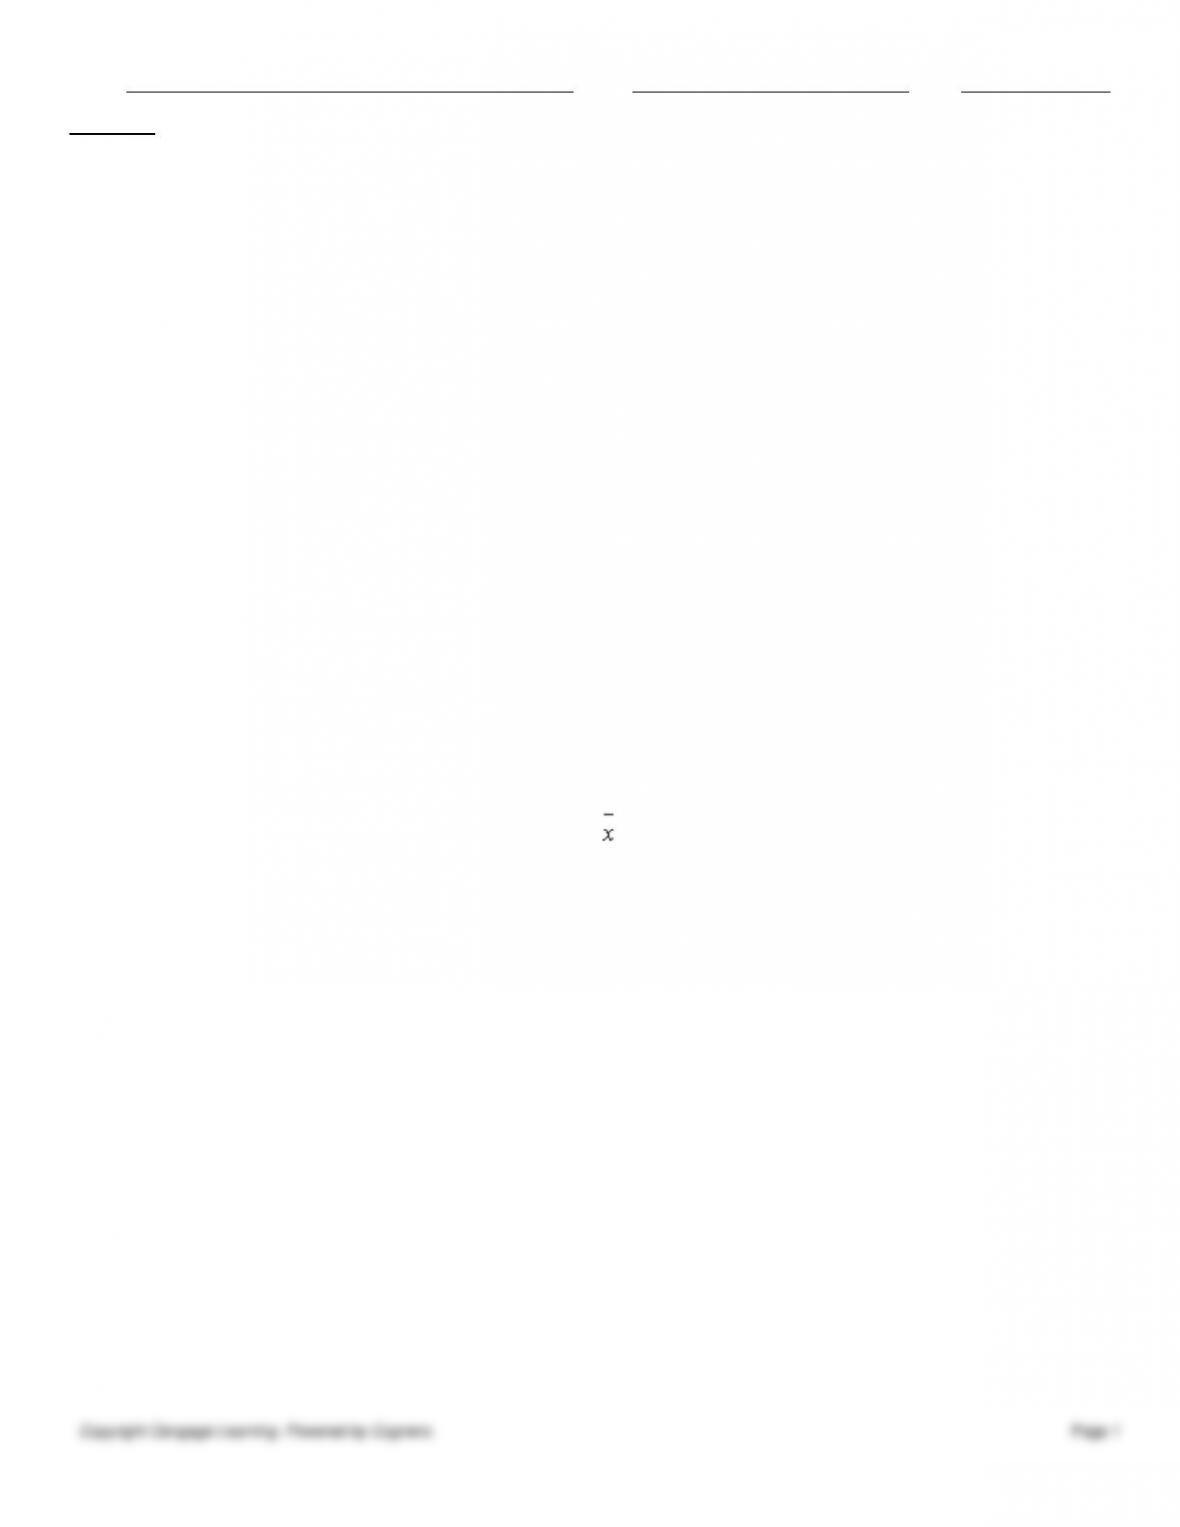
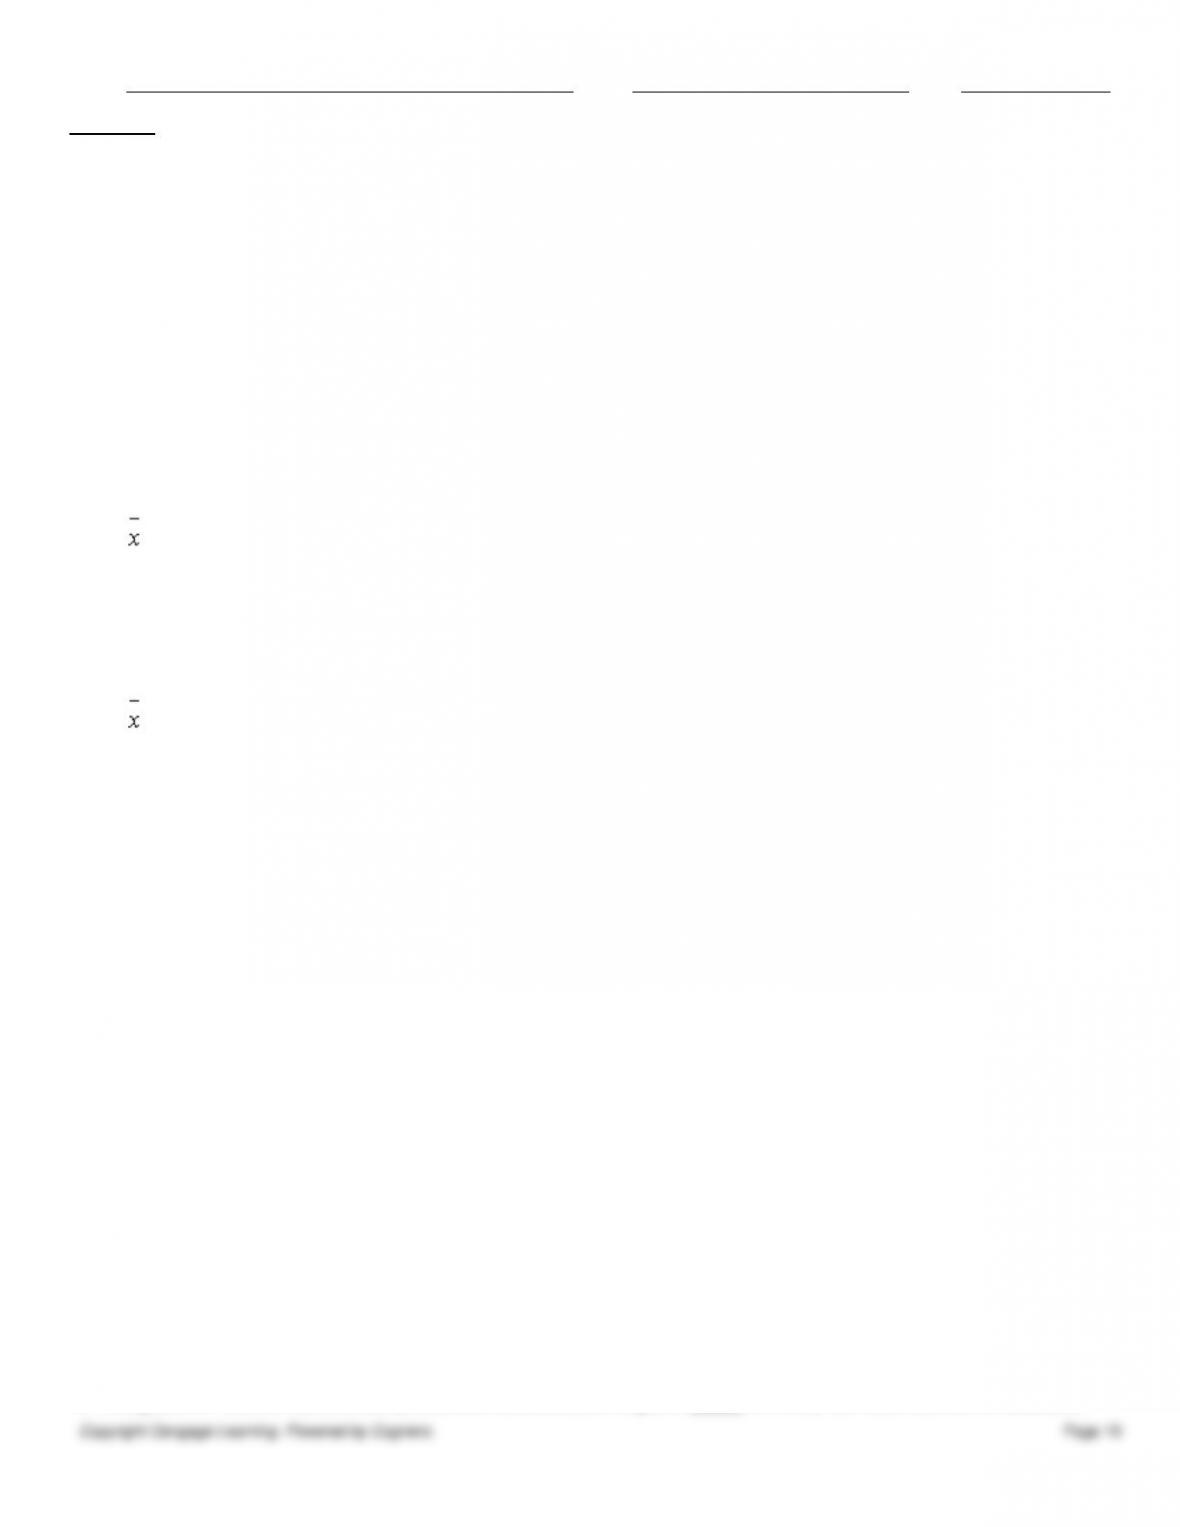
6. Process capability indexes can be computed from data in an -chart.
a.
True
b.
False
7. The total observed variation in production output is the sum of the true process variation plus variation due to
measurement.
a.
True
b.
False
8. If most of the points on a control chart fluctuate randomly between the control limits with no recognizable pattern, then
the process is in statistical control.
a.
True
b.
False
9. A c-chart is based on the binomial distribution.
a.
True
b.
False
10. Rolled throughput yield is the proportion of conforming units that results from a series of process steps.
a.
True
b.
False
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 2
11. A histogram of data that resembles the normal distribution indicates that the process is in control.
a.
True
b.
False
12. Common and special causes of variation must be eliminated before process capability can be determined.
a.
True
b.
False
13. For variable data, the two important quality measures are the proportion nonconforming and nonconformances per
unit.
a.
True
b.
False
14. Histograms allow you to distinguish between common and special causes of variation.
a.
True
b.
False
15. The center line for the np–chart is the average number of nonconforming items per sample.
a.
True
b.
False
16. The larger the sample size, the narrower the control limits.
a.
True
b.
False
17. If points on a control chart are determined to be the result of special causes, the points should be eliminated, and new
control limits should be computed.
a.
True
b.
False
18. A p-chart is used with the attribute data.
a.
True
b.
False
19. If the cost of investigating an operation to identify the cause of an apparent out-of-control condition is low, narrower
control limits should be selected.
a.
True
b.
False
20. A measurement system may be precise but not necessarily accurate at the same time.
a.
True
b.
False
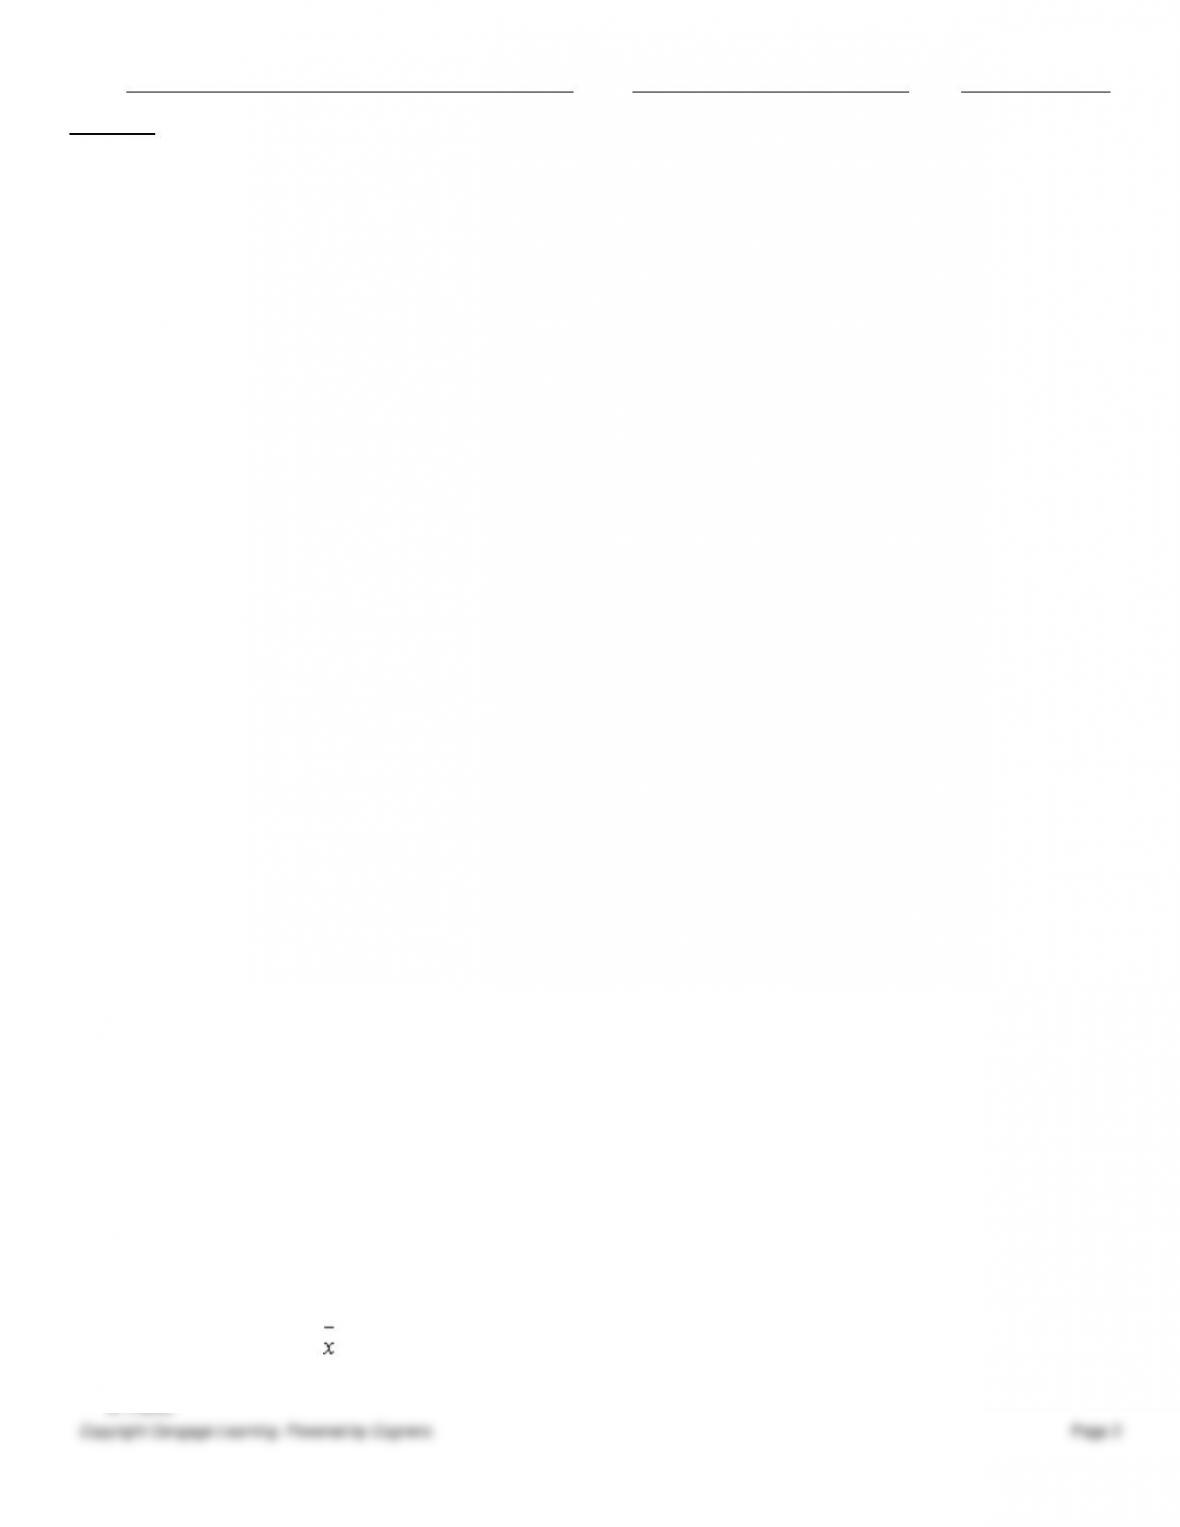
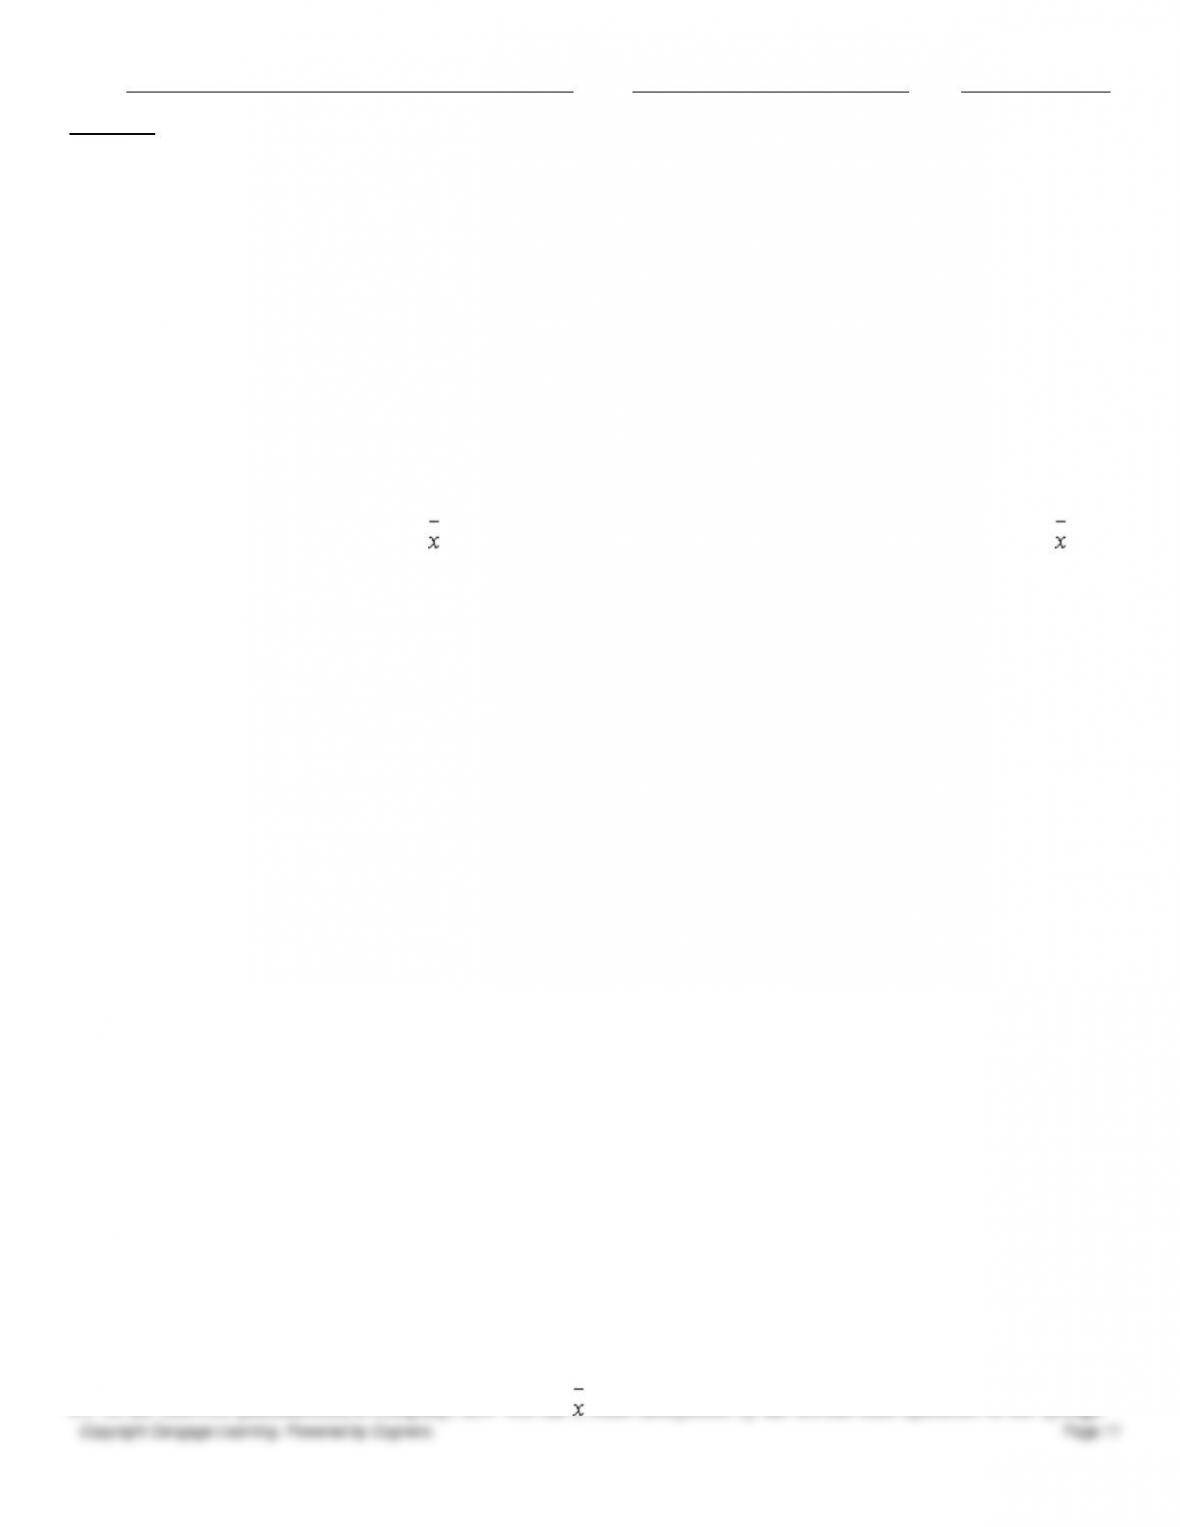
21. A better alternative to the -chart to monitor variation is to compute and plot the standard deviation s of each sample.
a.
True
b.
False
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 3
22. A “hugging the center line” pattern in a control chart can be the result of taking each sample from a different process
but not mixed together.
a.
True
b.
False
23. When constructing a u-chart, the standard deviation of each sample varies because the size of the sampling unit varies.
a.
True
b.
False
24. Attribute measurement requires a much larger sample size than variable measurement to obtain the same amount of
statistical information.
a.
True
b.
False
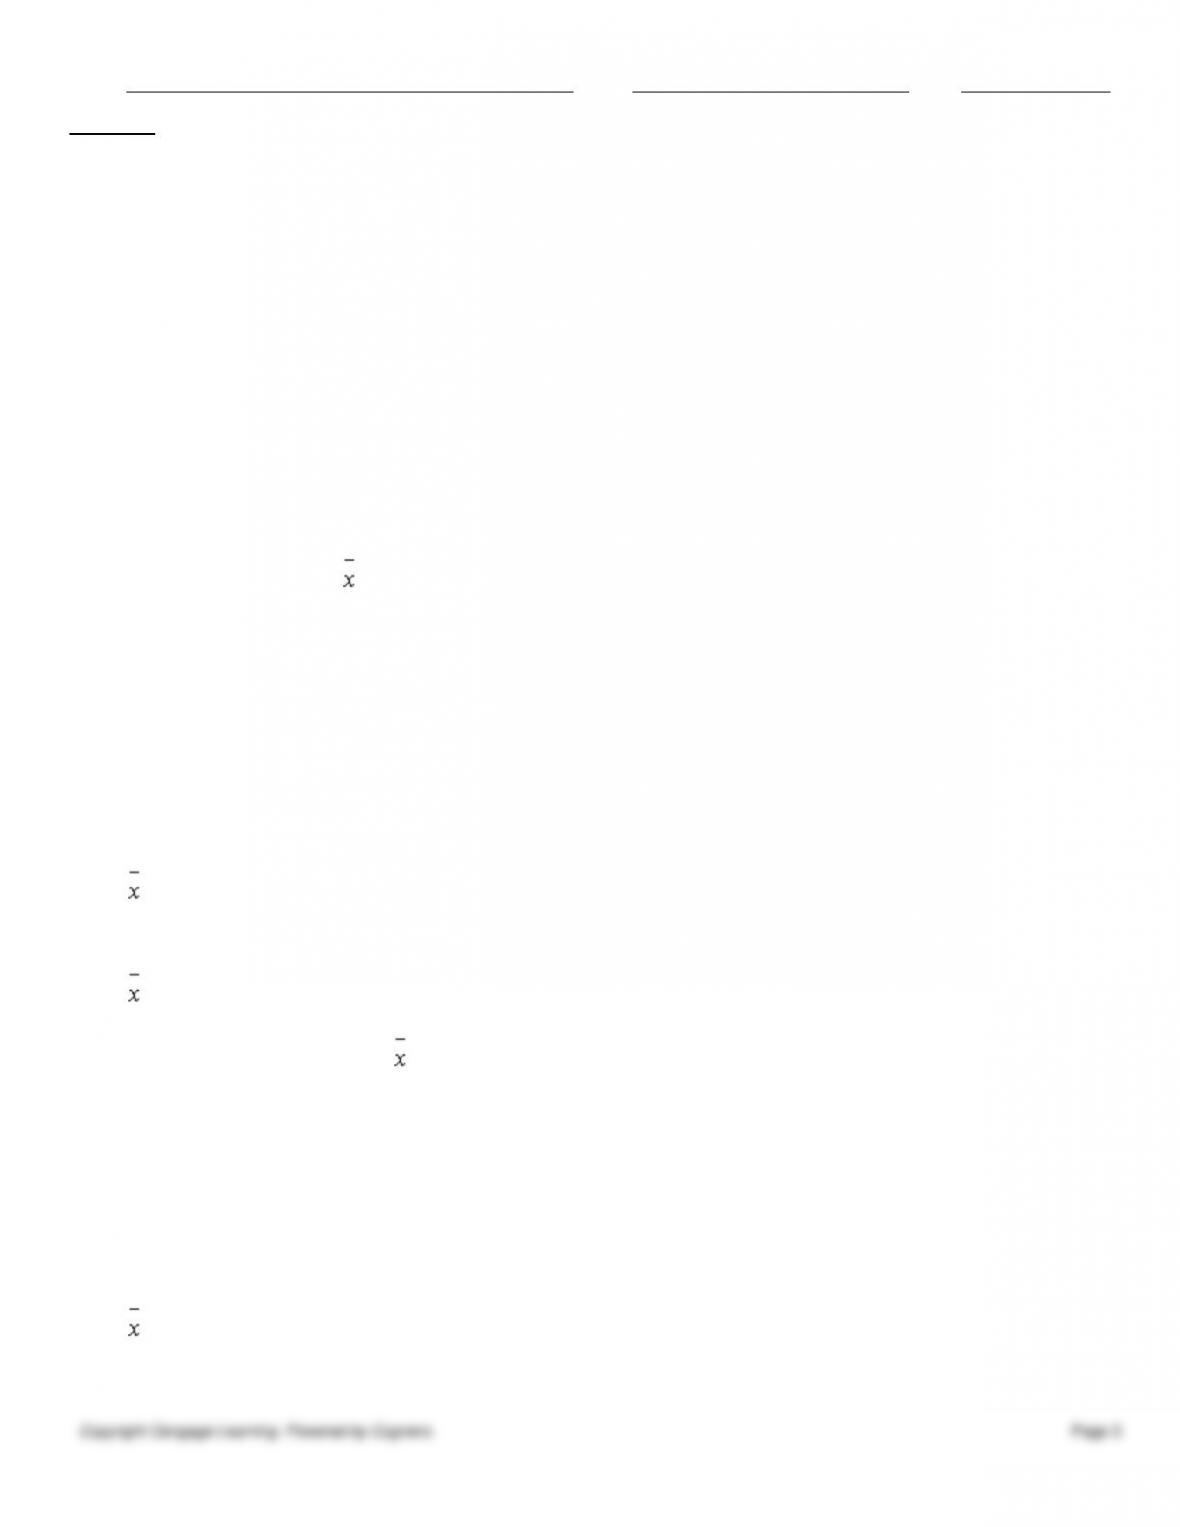
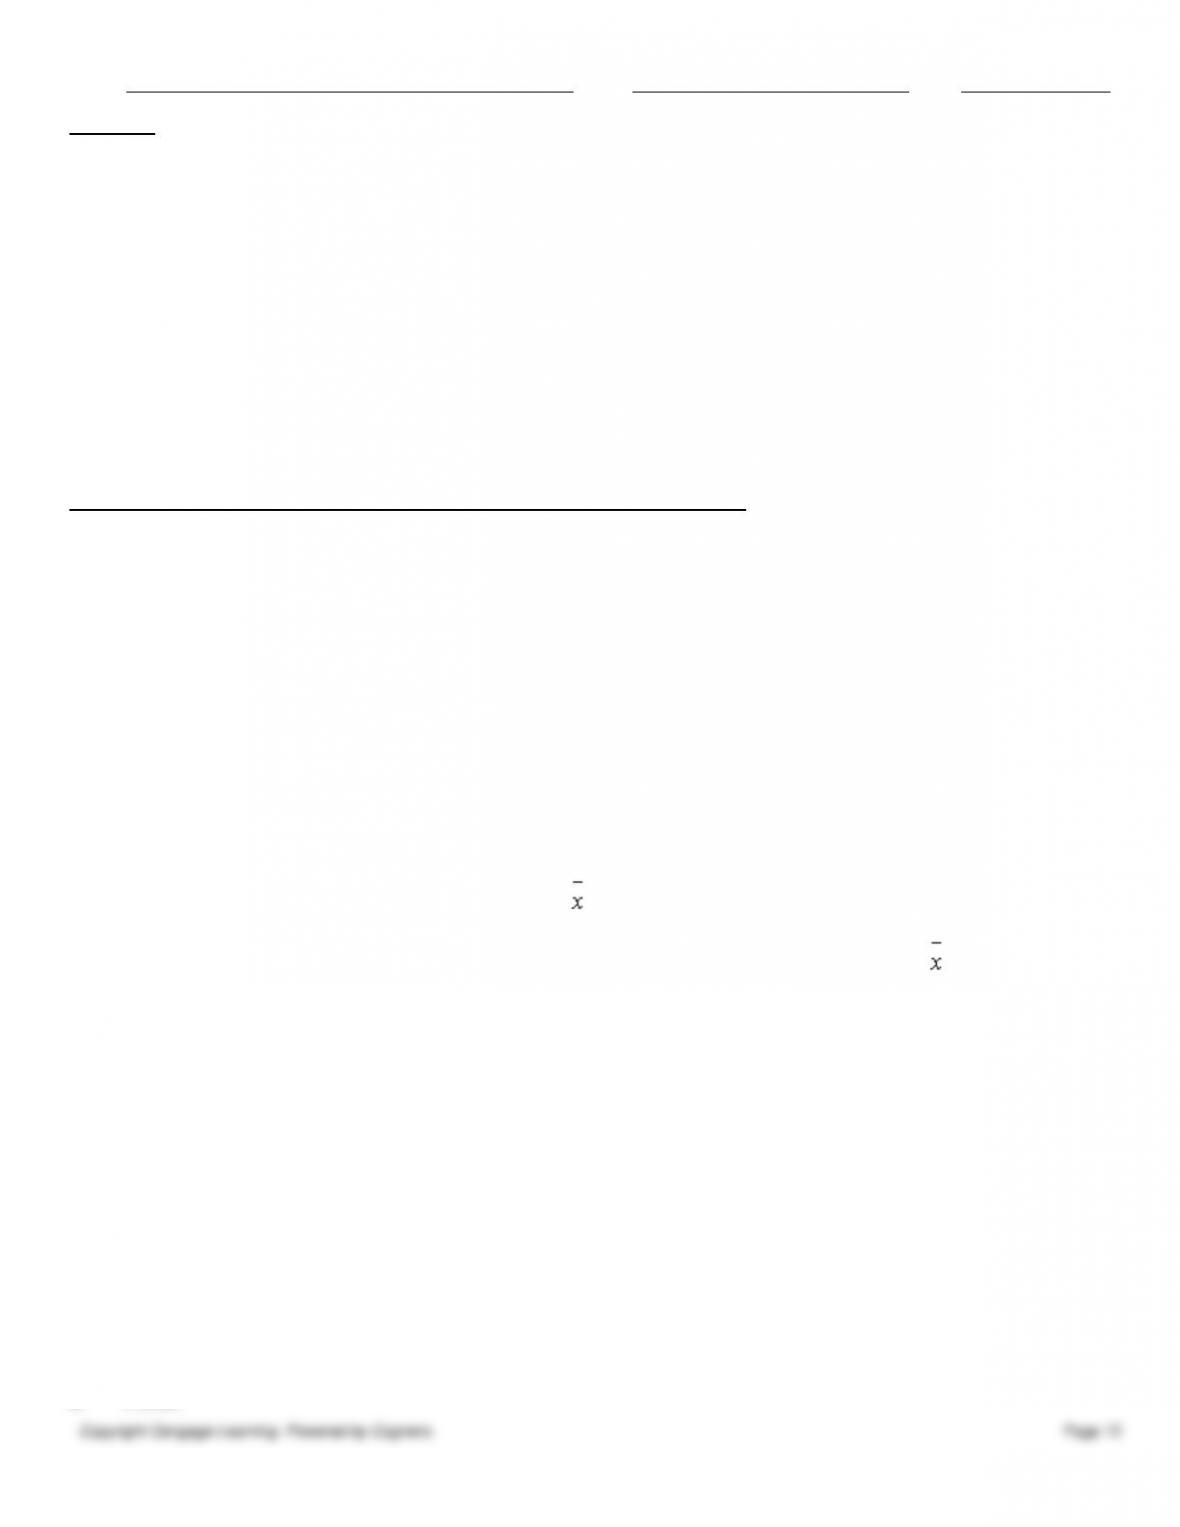
25. If all sample averages on an -chart fall within the control limits, all output will be conforming.
a.
True
b.
False
26. A nonconforming unit of work is one that has no defects or errors.
a.
True
b.
False
Indicate the answer choice that best completes the statement or answers the question.
27. Which of the following pairs of charts are used together?
a.
-chart and p-chart
b.
R-chart and p-chart
c.
R-chart and s-chart
d.
-chart and R-chart
28. To form rational subgroups for an -chart, the goal is to choose samples that are as _____ as possible.
a.
heterogeneous
b.
homogeneous
c.
large
d.
systematic
29. In determining whether a process is in statistical control, the _____ should be analyzed first.
a.
R-chart
b.
upper and lower control limits
c.
-chart
d.
center line
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 4
30. Control limits are often confused with
a.
pre-control lines.
b.
center lines.
c.
specification limits.
d.
three sigma limits.
31. Which of the following is a likely cause of the control chart pattern known as a trend?
a.
Aging of equipment
b.
Maintenance schedules
c.
New process operator
d.
Sudden power surge
32. Which of the following is NOT one of the basic applications of a control chart?
a.
To establish a state of statistical control.
b.
To calculate the average range.
c.
To monitor a process to identify special causes of variation.
d.
To determine process capability.
33. A better alternative to using the R-chart to monitor variation is the
a.
np-chart.
b.
s-chart.
c.
c-chart.
d.
p-chart.
34. Which of the following is NOT an indication of an out-of-control process?
a.
Five consecutive points fall on one side of the center line.
b.
Four of five consecutive points fall within the outer two-thirds region between the center line and one of the
control limits.
c.
Two of three consecutive points fall in the outer one-third region between the center line and one of the
control limits.
d.
A single point falls above the upper control limit.
35. Which of the following statements regarding an x-chart is true?
a.
Individual data require averaging before being plotted on it.
b.
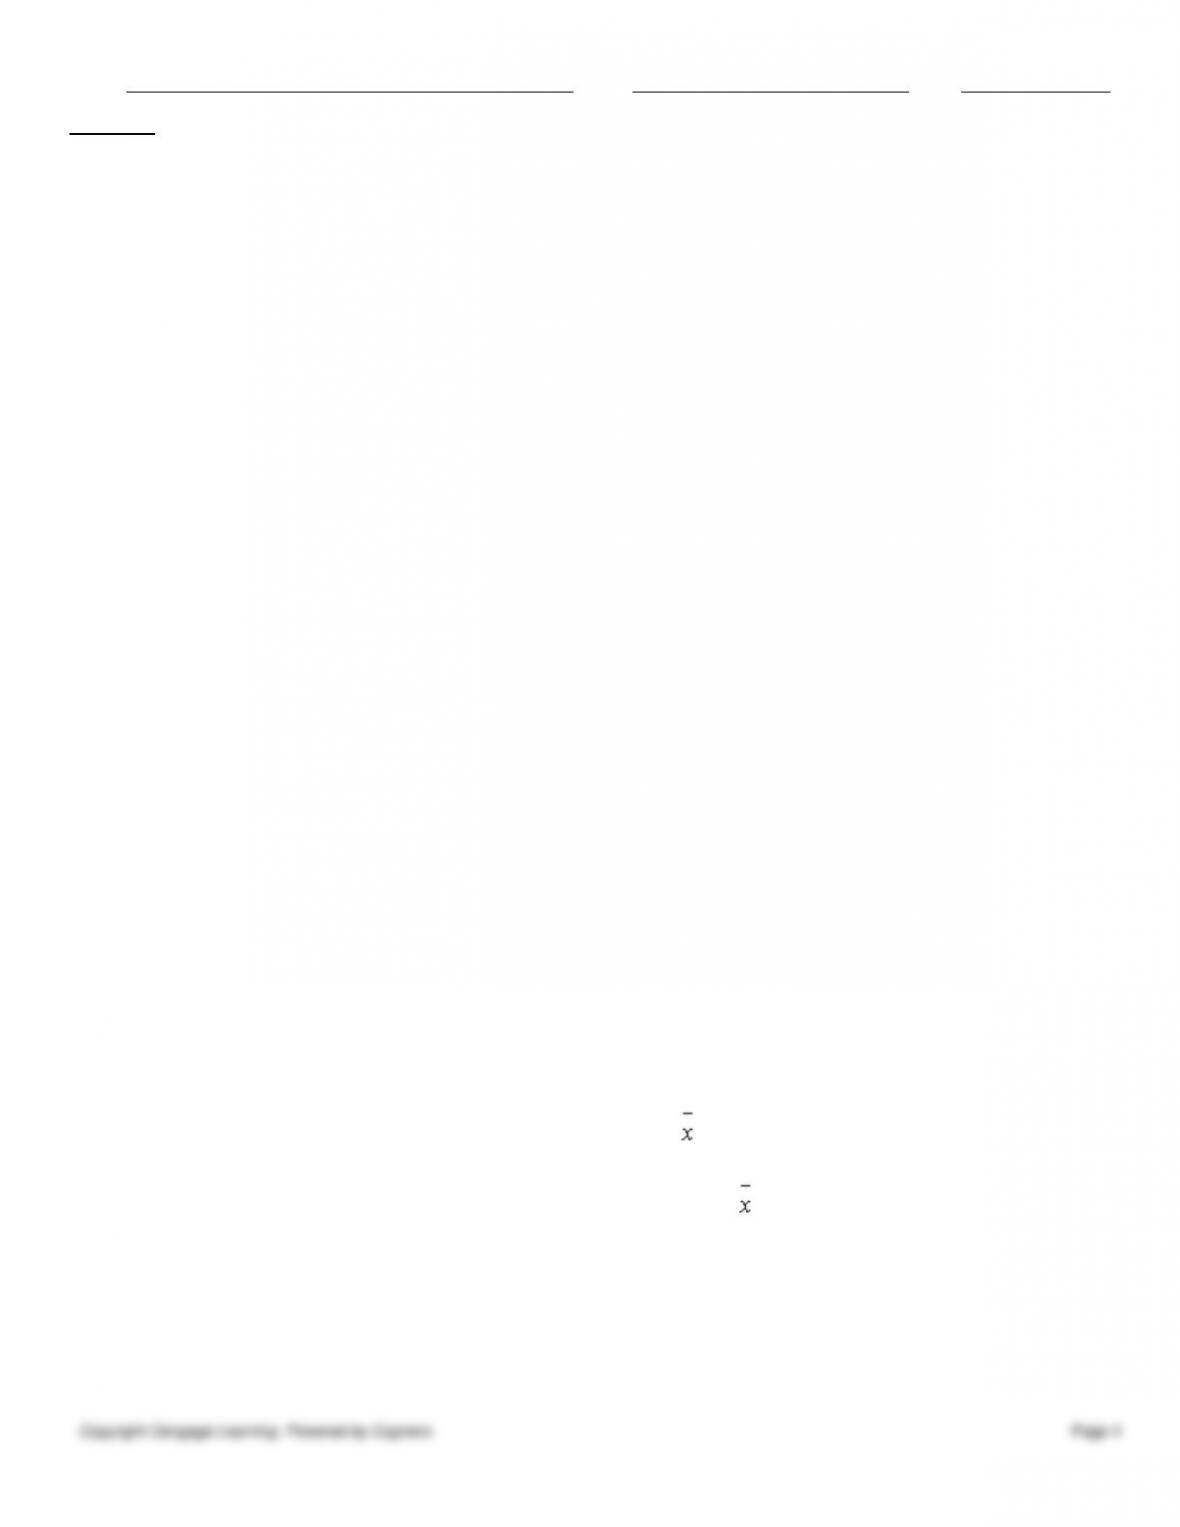
It is less sensitive to many conditions that can be detected by the -chart and R-chart.
c.
Specification limits cannot be drawn on the chart for direct comparison with the control limits.
d.
The assumption of normality of observations is less critical than for the -chart and R-chart.
36. A(n) _____ measurement characterizes the presence or absence of nonconformances in a unit of work.
a.
variable
b.
indicator
c.
attribute
d.
error
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 5
37. A process is said to be out of control when
a.
common causes are present.
b.
special causes are present.
c.
the process is not capable of meeting specifications.
d.
the upper and lower control limits cannot be computed.
38. All else being constant, if the sample size in a p-chart increases from 100 to 120, the upper and lower control limits
will
a.
move farther apart.
b.
move closer together.
c.
not be affected.
d.
both shift upward.
39. Which of the following charts is used to monitor the average number of nonconformances per unit when sample sizes
vary?
a.
–chart
b.
u-chart
c.
p-chart
d.
c-chart
40. A precision parts manufacturer produces bolts for use in military aircraft. The specifications for bolt length are 37.50 ±
0.25 cm. The company has established an –chart and an R-chart using samples of size five. The center lines for the –
chart and R-chart are set at 37.35 cm and 1.05 cm, respectively. Which of the following is the value of Cpk for this
process?
a.
0.07
b.
0.28
c.
0.75
d.
0.03
41. The control chart most appropriate for plotting the daily percentage of students that wait longer than 5 minutes in line
at the undergraduate admissions office is a(n)
a.
p-chart.
b.
np-chart.
c.
x-chart.
d.
-chart.
42. Six samples of size 10 were collected. The data are provided in the following table:
Sample number
1
2
3
4
5
6
Sample mean
4.80
4.62
4.81
4.55
4.92
4.65
Sample standard deviation
0.35
0.33
0.31
0.35
0.37
0.39
The upper control limit (UCL) and lower control limit (LCL) for an s-chart are
a.
LCL = 0.2840, UCL = 1.7160.
b.
LCL = 0.0994, UCL = 0.6006.
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 6
c.
LCL = 4.6256, UCL = 5.3256.
d.
LCL = 3.6750, UCL = 5.7750.
43. The output of a process is stable and normally distributed. If the process mean equals 23.5, the percentage of output
expected to be less than or equal to the mean
a.
is less than 25 percent.
b.
is 50 percent.
c.
is greater than 75 percent.
d.
cannot be determined without knowing the standard deviation value.
44. Variable data are
a.
discrete.
b.
not measurable.
c.
continuous.
d.
nonrandom.
45. A c-chart is based on the _____ probability distribution.
a.
normal
b.
binomial
c.
Poisson
d.
exponential
46. The sample size for an x–chart
a.
should be between 25 and 30.
b.
is larger than that for an -chart.
c.
is equal to one.
d.
should be greater than one.
47. Each day, a manufacturing company producing circuit boards will randomly sample 60 circuit boards for a period of
25 days and then determine and plot the number of defects contained in each of these boards. The appropriate control
chart is a(n)
a.
u-chart.
b.
p-chart.
c.
np-chart.
d.
c-chart.
48. Defects per million opportunities (dpmo) =
a.
(Number of defects discovered)/Opportunities for error × 100,000.
b.
(Number of defects discovered)/Opportunities for error × 1,000,000.
c.
(Opportunities for error × Number of defects discovered)/1,000,000.
d.
(Opportunities for error/Number of defects discovered) × 10,000,000.
49. Twenty samples of size 6 were collected for a variable measurement. Which of the following is the upper control limit
(UCL) and lower control limit (LCL) for an R-chart if the sum of the sample ranges equals 88.0?
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 7
a.
UCL = 8.8176; LCL = 0.0000
b.
UCL = 9.3016; LCL = 0.3344
c.
UCL = 13.2000; LCL = 0.0000
d.
UCL = 29.3921; LCL = 0.0000
50. In service applications, the term _____ is generally used to describe a nonconformance.
a.
cycle
b.
unit
c.
error
d.
trend
51. If a process is neither capable nor in control, the appropriate first step is to
a.
remove common causes of variation.
b.
redesign the equipment.
c.
remove special causes of variation.
d.
determine the process capability index.
52. The s-chart is recommended when
a.
the control chart calculations need to be performed by hand.
b.
tight control of variability in the process is required.
c.
the -chart is not associated with an R-chart.
d.
the sample size for each sample needs to be reduced.
53. Short, repeated patterns in a control chart, with alternating high peaks and low valleys, are known as
a.
trends.
b.
cycles.
c.
shifts.
d.
runs.
54. Assuming 25 samples of size 100 were collected and a total of 96 nonconforming items were found, the upper control
limit for the p-chart would be
a.
0.083.
b.
0.096.
c.
0.137.
d.
0.254.
55. _____ is a study of variation in a measurement system using statistical analysis.
a.
A metrology study
b.
An SPC study
c.
A repeatability and reproducibility (R&R) study
d.
A calibration study
56. If the variation in the process is due to common causes alone, the process is said to be
a.
out of control.
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 8
b.
in pre-control.
c.
in statistical control.
d.
out of capability.
57. Which of the following statements regarding a major advantage of np-charts is true?
a.
They can be used for variable sample sizes.
b.
They are more accurate than p-charts.
c.
They are easier to understand for production personnel than p-charts.
d.
The control limits are based on binomial distribution.
58. Because of high test costs, a sample of single wastewater sludge is tested daily for dissolved oxygen content. The
appropriate control chart(s) would be
a.
-chart and R-chart.
b.
u-chart.
c.
x-chart and moving range chart.
d.
x-chart and R-chart.
59. A machined part has a lower specification limit of 3.5 inches and an upper specification limit of 3.9 inches. The range
for the pre-control green zone is
a.
3.6 inches to 3.8 inches.
b.
3.8 inches to 3.9 inches.
c.
less than 3.5 inches.
d.
3.5 inches to 3.9 inches.
60. A(n) _____ monitors the fraction of nonconforming units.
a.
c-chart
b.
u-chart
c.
np-chart
d.
p-chart
61. A delivery company defines a defect as a package delivered later than the promised delivery time. Management wants
to monitor the proportion of such defect packages per week and plans to sample 120 packages every week. The
appropriate control chart is a(n)
a.
-chart.
b.
R-chart.
c.
p-chart.
d.
np-chart.
62. A preliminary analysis involving data entry at the featured distributor of electrical automation and power transmission
products revealed that packing slips contained errors; to remedy this problem, a _____ was constructed for each day to
track the number of defects found.
a.
Quality Assurance Committee
b.
sampling strategy
c.
u-chart
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 9
d.
new production process
63. If the process mean and variance do not change over time, the process is
a.
in statistical control.
b.
normally distributed.
c.
stable.
d.
capable.
64. For variables data, the sample means are assumed to be
a.
exponentially distributed.
b.
normally distributed.
c.
Poisson distributed.
d.
binomially distributed.
65. Statistical process control relies on
a.
process capability studies.
b.
dashboards.
c.
control charts.
d.
metrology.
66. The x-chart is used for
a.
averages of variables data.
b.
individual attributes data.
c.
individual variables data.
d.
averages of attributes data.
67. A _____ is the result of some cause that gradually affects the measurement and causes the points on a control chart to
gradually move up or down from the center line.
a.
defect
b.
process shift
c.
cycle
d.
trend
68. A canning company defines a “nonconformance” as an orange juice can whose diameter is beyond the upper
specification limit. A manager at the canning company wants to monitor the number of such orange juice cans produced
per day. Each day, an employee will randomly select 120 cans over a period of four weeks. The employee then determines
and plots the number of nonconformance cans in each sample. The appropriate control chart is a(n)
a.
u-chart.
b.
R-chart.
c.
p-chart.
d.
np-chart.
69. After the featured distributor of electronic automation and power transmission products consolidated the types of
packing slip errors into five categories, a _____ was performed.
a.
price evaluation
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 10
b.
Pareto analysis
c.
qualification standard
d.
quantification
70. _____ is measured as the amount of error in a measurement in proportion to the total size of the measurement.
a.
Precision
b.
Accuracy
c.
Systematic bias
d.
Capability
71. A company wishes to monitor the variation in the length of time it takes to process and send a bill to a customer.
Seven bills will be randomly selected each day for a 60-day period and the length of time it takes to process and send the
bill to a customer will be recorded for each bill. The appropriate control chart is a(n)
a.
-chart.
b.
R-chart.
c.
p-chart.
d.
u-chart.
72. The _____ is used to monitor the centering of the process.
a.
-chart
b.
R-chart
c.
p-chart
d.
np-chart
73. For statistical process control, a good sampling method should always
a.
use samples of random measurements over a long period of time.
b.
minimize sampling cost.
c.
maximize sample size.
d.
use rational subgroups.
74. Collecting _____ data is usually easier than collecting _____ data because the assessment can usually be done more
quickly by a simple inspection or count.
a.
variable; attribute
b.
conformances; nonconformances
c.
attribute; variable
d.
simple; complex
75. In pre-control, which of the following zones covers the nominal specifications of a process?
a.
Gray zone
b.
Green zone
c.
Red zone
d.
Yellow zone
76. Compared to variable measurement, attributes measurement requires _____ to obtain the same amount of statistical
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 11
information about the quality of the product.
a.
a more distributed population
b.
more nonconformances
c.
a much larger sample size
d.
a smaller sample size
77. Process capability calculations make little sense if the process
a.
data were taken over time.
b.
is not in statistical control.
c.
variations are due to common causes.
d.
is not initiated.
78. A precision parts manufacturer produces bolts for use in military aircraft. The specifications for bolt length are 37.50 ±
0.25 cm. The company has established an -chart and an R-chart using samples of size five. The center lines for the –
chart and R-chart are set at 35.25 cm and 1.08 cm, respectively. Which of the following is the value of Cp for this process?
a.
1.333
b.
0.179
c.
0.301
d.
0.166
79. In an attempt to solve the problem of tacked syringes at a Midwest pharmaceutical product manufacturer, statistical
consultants recommended _____ for the purpose of improving the tacking operation.
a.
ANOVA
b.
pre-control
c.
measurement system evaluation
d.
statistical process control (SPC)
80. If the lower limit for a p–chart computes to a number less than zero, this indicates that
a.
the lower limit should be set at zero.
b.
the process is out of control.
c.
an attribute measure is incorrectly used.
d.
a calculation error has been made.
81. What did the statistical consultants recommend to the managers of the Midwest pharmaceutical company after the
maintenance technician explained the reason for the increased length of the syringes? Was the recommendation
implemented? What was the result?
82. The featured distributor of electrical automation and power transmission products implemented a total quality
program. Describe its effect on the distributor’s receiving process.
83. At the Midwest pharmaceutical company, what conclusions were drawn by the statistical consultants using the R–
chart?
84. At the Midwest pharmaceutical company, how was the -chart interpreted by the second shift operators of the syringe
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 12
assembly process after the machine had been adjusted three times by the technician? How did the statistical consultants
interpret it?
85. State the conclusion drawn by the operators in the capability study of the tacking operation at the Midwest
pharmaceutical company.
86. Define the term “statistical process control.” Outline the steps for setting up a control chart to monitor a process.
87. A process fills boxes with detergent. Construct an appropriate set of control limits to monitor the filling process.
Historical data for fill weight (in ounces) of 10 samples are presented in the table that follows. A sample size of six was
used.
Sample
Sample Mean
Sample Range
1
15.80
0.42
2
16.10
0.38
3
16.02
0.08
4
15.95
0.15
5
16.12
0.42
6
16.18
0.23
7
15.87
0.36
8
16.20
0.40
9
16.07
0.28
10
15.94
0.36
88. Define pre-control, and explain under what conditions pre-control can be used.
89. In the production of vitamin capsules, the proportion of calcium in each capsule has a specification of 48 ± 18 parts
per million (ppm). An initial random sample of 100 capsules revealed a sample average calcium content of 44.5 ppm and
a sample standard deviation of 3.2 ppm. Management uses – and R-charts to monitor the calcium amount using samples
of size 4 for each.
The charts depict an in-control process. The center line of the R-chart is 6.7 and the center line of the -chart is 44.8.
a. Compute Cp for this process using estimates of the process mean and standard deviation derived from the random
sample.
b. Compute Cp for this process using estimates of the process mean and standard deviation derived from the control chart
parameters.
c. Compute Cpk for this process using estimates of the process mean and standard deviation derived from the random
sample.
d. Compute Cpk for this process using estimates of the process mean and standard deviation derived from the control
chart parameters.
e. What do the differences between the values of Cp and Cpk tell you?
90. Define each of the following control chart patterns. Include a sketch for patterns b through f with your definition.
a.
One point outside the control limits
b.
Sudden shift in the process average
c.
Cycles
d.
Trends
Name:
Class:
Date:
chapter 8
Copyright Cengage Learning. Powered by Cognero.
Page 13
e.
Hugging the center line
f.
Hugging the control limits
91. Coils of synthetic rope are monitored for defects. Each coil contains 1,200 feet of rope. There were 26 coils selected,
and the number of defects found in each coil is presented in the table that follows. Identify an appropriate control chart,
and determine the chart’s control limits.
Sample
Number of Defects
Sample
Number of Defects
1
1
14
0
2
3
15
5
3
4
16
4
4
2
17
2
5
4
18
3
6
2
19
0
7
0
20
3
8
3
21
4
9
2
22
3
10
2
23
1
11
1
24
2
12
4
25
0
13
3
26
3
92. RM Industries wishes to monitor its end-of-week accounts receivable balance. To do so, the end-of-week balances for
the previous 25 weeks were recorded and are shown in the table that follows. Establish an x-chart and a moving range
(using n = 2) chart for this process.
Week
Balances (in thousands)
Week
Balances (in thousands)
1
37.10
14
54.75
2
51.75
15
50.44
3
61.91
16
60.77
4
27.44
17
38.22
5
37.39
18
29.17
6
31.43
19
65.26
7
49.21
20
53.46
8
26.19
21
37.67
9
43.96
22
53.24
10
33.97
23
59.60
11
47.09
24
20.18
12
56.06
25
49.67
13
46.13
93. Identify the trade-offs associated with the s–chart instead of the R-chart.
94. A bank recently took 32 random samples of size 600 to determine the accuracy of its customer records. A customer
record was nonconforming if any portion of the record was left blank. The sample data are presented in the table that
follows. Determine the control limits for an np–chart.
Sample
Number Nonconforming
Sample
Number Nonconforming
1
21
17
20
2
22
18
16
3
20
19
11
4
21
20
24